


Standard granite bases can hardly meet the customized demands of non-standard inspection equipment. Many special inspection equipment development projects encounter troubles such as mismatched mounting holes, conflicting wiring groove positions and misaligned sensor mounting surfaces. If users forcibly adopt standard bases and carry out secondary on-site machining, the original flatness of the reference surface will easily be damaged and new stress deformation will be introduced. With the ultra-precision granite component processing capability, UNPARALLELED Group adopts integrated pre-process slotting, drilling and multi-face precision machining. Custom structural machining is finished in the factory workshop to produce integrated granite bases for various non-standard inspection equipment.
Pre-customized design to coordinate reference surface and structural features of the base The difficulty of non-standard equipment lies in that its structure, sensors and motion module layout are all uniquely designed, with no universal templates for the position, depth and size of mounting holes, wiring grooves and avoidance notches. The conventional method is to machine the reference plane first and drill holes on site later. Impact and thermal effects generated by drilling will damage the reference surface and degrade flatness. In the early stage of projects, UNPARALLELED Group collaborates with equipment R&D teams to integrate all mounting holes, wiring grooves, module avoidance grooves and positioning steps into the overall machining model of the base. Rough slotting and hole forming are completed in the rough machining stage, followed by static aging for stress release before ultra-precision grinding of the reference surface. This processing sequence prevents damage to the reference flatness caused by slotting and drilling.
Precision machining of special holes and grooves on granite to balance dimensional accuracy and stone protection Granite features high hardness and brittleness. Ordinary metal machining tends to cause edge chipping and subsurface microcracks, undermining the long-term stability of the base. Through holes, countersunk mounting holes, pre-embedded threaded holes, long wiring grooves and sensor avoidance grooves require different tools, cutting parameters and cooling schemes. UNPARALLELED Group uses special diamond cutting tools for granite, controls cutting feed rate to reduce machining impact, and minimizes edge chipping and invisible subsurface microcracks. Hole walls and groove walls are finely polished to guarantee the tolerance of hole spacing, groove width, parallelism and position for equipment assembly, while protecting the integrity of stone substrates and preventing holes and grooves from becoming stress concentration points.
Multi-face coordinated machining to guarantee geometric tolerances between holes/grooves and reference surface During assembly of non-standard inspection equipment, not only the flatness of the plate surface needs to meet standards, but also the perpendicularity, parallelism and positional tolerance between hole axes, groove sides and the reference surface determine the assembly precision of sensors, probes and linear motor modules. Separate slotting, drilling and reference grinding easily cause geometric deviation, leading to tilted module assembly and zero drift of probes. Equipped with large-scale CNC equipment, UNPARALLELED Group completes multi-face machining of the base under one-time clamping, locking all holes and grooves in a unified coordinate system together with the main reference surface. After full machining, high-precision measuring instruments are adopted for grid inspection of hole spacing and geometric tolerances of grooves, ensuring stable geometric relationship between all customized structures and the main reference surface.
Adapt to complex integration requirements and reserve space for equipment assembly and maintenance Non-standard inspection equipment usually integrates optical components, XY motion stages, air source pipelines, cables and air bearing guides. The granite base acts not only as a bearing platform but also as an integrated carrier for the whole machine. According to equipment drawings, UNPARALLELED Group can machine cable embedding grooves, air pipe avoidance grooves, weight reduction grooves, positioning pin holes and locking counterbores for modules inside the base. Integrated slotting and drilling allow hidden cable routing, reduce interference between external cables and moving parts, simplify overall assembly and keep the base neat. For equipment such as semiconductors, AOI and lithium battery inspection, assembly stations for components can also be reserved to facilitate commissioning and later maintenance of the complete machine.
Stress control and full-dimensional inspection after customized machining Slotting and drilling will introduce new machining stress inside granite. Without proper treatment, stress will be released gradually in service and deform the reference surface. After all slotting and drilling procedures, UNPARALLELED Group carries out special constant-temperature static aging to release residual stress generated by hole and groove machining. Only after deformation stabilizes can final fine grinding of the reference surface start. In finished product inspection, we test not only plate flatness but also hole coordinate, groove dimension and geometric tolerances. All measuring instruments are traceable to national metrology institutes, ensuring both the reference precision of the base and the dimensional accuracy of customized structures meet long-term operating requirements of non-standard equipment.
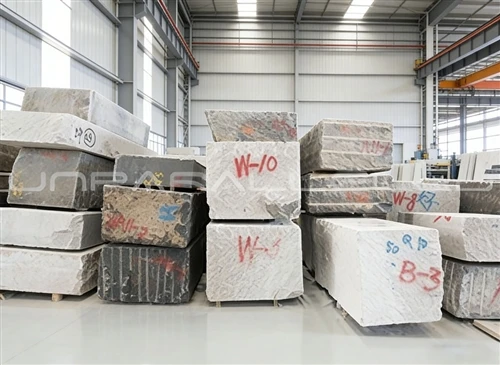
Integrated machining capability for large-sized non-standard bases Some large non-standard inspection equipment requires extra-long and extra-wide granite bases, which put high demands on the travel of slotting and drilling. UNPARALLELED Group owns large CNC machining equipment to process heavy and large granite blanks, realizing one-time slotting and multi-hole array drilling for extra-long bases and avoiding seam errors brought by multi-section splicing. From drawing communication, process review, blank preparation, slotting and drilling, aging treatment and ultra-precision grinding to full-dimensional inspection, one-stop delivery is available. Customers are freed from outsourcing secondary machining after purchasing standard bases, lowering precision risks and project cycle costs brought by repeated processing.