


Many high-precision optical sensing systems suffer from signal jumps and poor repeatability during commissioning. Troubleshooting light sources, lenses and detectors often fails to identify the root cause, which frequently lies within the stage base itself. If the base substrate carries magnetism or retains residual magnetism after machining, stray magnetic fields will form around sensing components. These fields disturb magneto-sensitive photoelectric sensors, polarization detection elements and interferometric sensing units, leading to drifting optical signals and even reduced detection resolution of equipment. The core value of a non-magnetic optical stage base is to eliminate such magnetic interference at the hardware source and keep optical sensor assemblies operating steadily. UNPARALLELED Group has developed a complete set of material selection, machining and inspection solutions for non-magnetic bases through numerous photoelectric sensing equipment projects.
1. Stray Magnetic Field: An Overlooked Interference Source for Optical Sensing
Optical sensing components are designed to capture extremely weak optical signals. Many photodetectors, polarization sensors and magneto-optical sensing chips are highly sensitive to surrounding magnetic fields. Engineers often instinctively select metal bases for their good rigidity and easy machining, yet metal materials carry hidden magnetic risks. After CNC cutting and heavy grinding, ordinary stainless steel undergoes metallographic changes on its surface and generates local residual magnetism. Ferrous alloys are inherently magnetic, and surface coating cannot fully isolate magnetic fields. The stray magnetic fields produced by such bases are invisible; they will not directly damage optical components but alter electron motion inside sensors, distort polarization states and cause irregular fluctuations in collected optical signals. Not all natural stone is safe either. Low-cost granite raw materials may contain abundant ferromagnetic minerals. Tiny ferromagnetic particles inside the stone create local magnetic spots. As the equipment vibrates over long periods, magnetic field stability shifts and disturbs optical sensing signals.
2. Material Selection Logic for Non-magnetic Bases: Magnetic Property Control Starts at Raw Material Stage, Not Only Finished Product Testing
To ensure the base does not interfere with optical sensors, non-magnetic performance management must be implemented at raw material screening rather than merely testing finished workpieces. When raw blanks of UNPARALLELED® non-magnetic granite enter the factory, batch magnetic screening is performed to reject materials with excessive ferromagnetic minerals, eliminating internal magnetic spots from the start. This selected natural granite is a mineral aggregate with no inherent magnetic permeability. Unlike metals, it will not develop machining-induced residual magnetism during cutting, grinding, grooving and other processing steps. Its chemical properties remain stable; it will not become magnetized with changing temperature and humidity, maintaining constant magnetic properties over long service life. Comparing alternative substrates: precision ceramics are also non-magnetic and suitable for small sensing modules. Mineral casting is non-magnetic but difficult to machine to nano-level reference flatness, making it unsuitable for high-precision optical sensing reference surfaces. Selected non-magnetic granite combines non-magnetic performance, capability for large-size fabrication, high flatness and vibration damping advantages, which makes it the preferred choice for medium and large optical sensing stages.
3. Machining and Assembly Control: Prevent Magnetic Contamination Introduced During Production
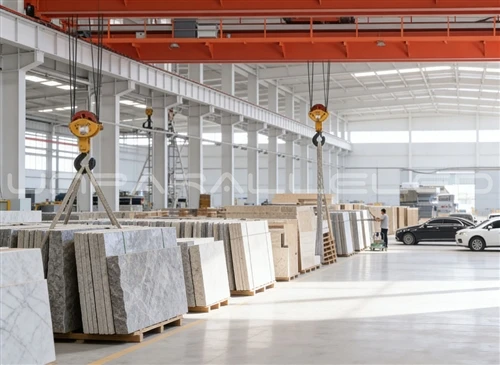
Even with non-magnetic raw materials, magnetic impurities may be introduced during machining and assembly to interfere with optical sensors. A common pitfall in non-magnetic projects occurs when iron chips and magnetic abrasives embed into stone pores and form scattered magnetic spots on the working surface of the base. UNPARALLELED sets up separate non-magnetic processing zones for non-magnetic base production. All cutting tools and polishing consumables adopt non-magnetic grades to prevent ferromagnetic debris from adhering to or embedding into the base. After finishing, in addition to conventional dimensional and flatness inspection, full-area multi-point magnetic field scanning is conducted, covering mounting areas, module fixing zones and key positions under optical paths to confirm no local residual magnetism exists. All matching assembly parts follow non-magnetic standards: locating pins, locking screws and leveling supports are non-magnetic fasteners to avoid magnetic interference originating from hardware components. Finished products are cleaned and packaged in a constant-temperature, constant-humidity dust-free workshop to prevent ferromagnetic dust from attaching to the surface during transportation.
4. Application for Various Optical Sensing Scenarios to Avoid Signal Abnormalities Caused by Magnetic Fields
Non-magnetic bases are suitable for various applications equipped with highly sensitive optical sensing assemblies: polarization optical inspection, laser interferometric sensing, quantum photoelectric detection, semiconductor wafer optical metrology and magneto-optical AOI inspection. In these scenarios, optical sensors continuously collect faint optical signals, and any minor magnetic disturbance will amplify noise. Adopting UNPARALLELED non-magnetic granite stage bases with matched non-magnetic fasteners creates a low-magnetic environment around optical sensing assemblies. It eliminates signal noise triggered by magnetic fields, ensuring authentic and stable data captured by sensors and reducing frequent recalibration requirements for equipment. Note that non-magnetic bases only resolve magnetic interference; they cannot replace vibration damping and thermal stability design. A complete optical stage system must simultaneously satisfy non-magnetic, vibration damping and dimensional stability requirements to fully release the performance limit of optical sensing components.
5. Maintenance Guidelines After Commissioning
After equipment deployment, maintenance should be performed to avoid magnetic contamination in later operation. Do not clean the base working surface with ordinary steel brushes or iron-containing grinding tools. Avoid direct impact or scratching on the tabletop with metal tools to prevent iron chips from embedding into pores. When disassembling optical sensing modules, use supporting non-magnetic tools. Recheck the magnetic field level on the table periodically, especially after large motors, transformers or other high-magnetic equipment are installed nearby in the workshop, to verify the working environment of optical sensors remains unaffected.
Conclusion
The signal stability of optical sensing assemblies depends not only on optical devices themselves; stray magnetic fields introduced by stage bases represent a non-negligible hidden interference. Upholding the quality policy that "For precision work, no amount of rigor is excessive", UNPARALLELED Group controls base magnetic performance across the full workflow, including raw material magnetic screening, non-magnetic processing management and finished-product magnetic testing. It supplies non-magnetic granite optical stage bases to eliminate stray magnetic interference on optical sensing assemblies and build a pure, stable optical reference for photoelectric measurement systems.